Is a reaction we often get and that is exactly the point.
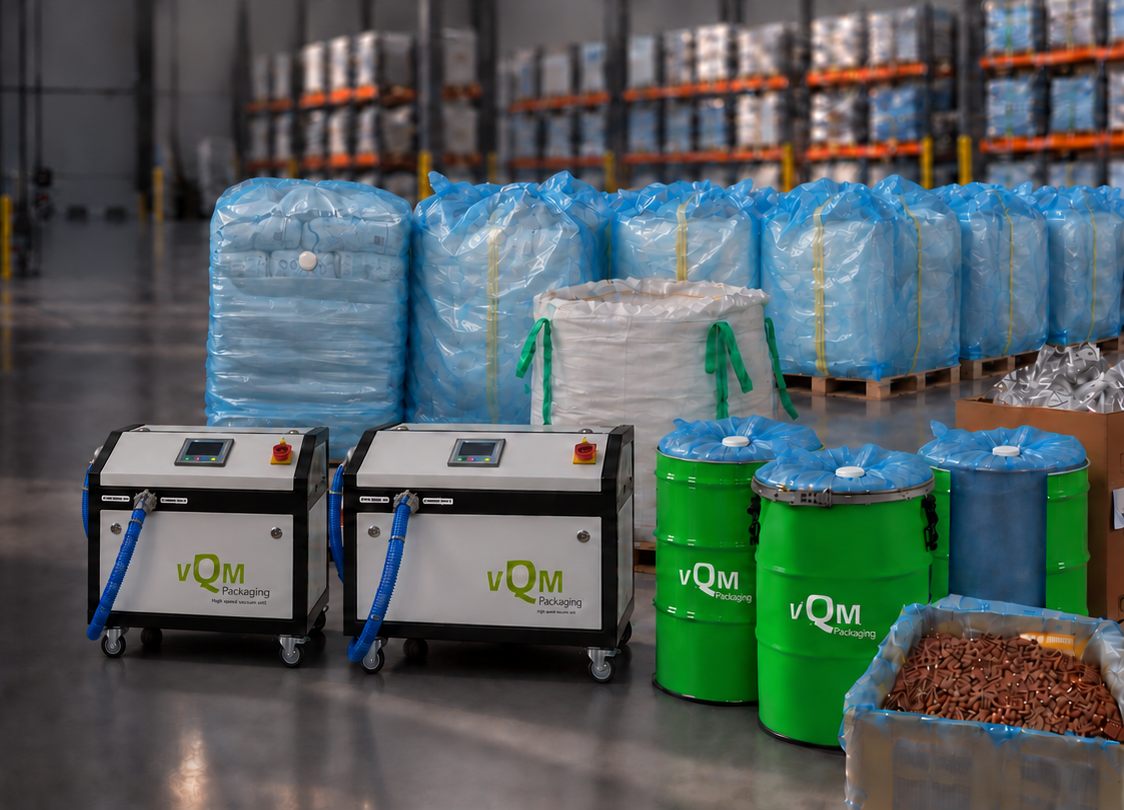
The principle behind our technology is straightforward: create the right conditions inside high-barrier packaging and protect the product throughout storage and transport.
Turning that simple principle into an extremely fast, reliable and scalable solution for pallet-sized and semi-bulk packaging took considerably more engineering.
Today, vQm combines patented valve technology, high-barrier packaging and dedicated vacuum and gas-flushing equipment to make Modified Atmosphere Packaging practical for products ranging from premium food commodities to agricultural seeds, powders and industrial materials.
Our philosophy has remained the same from the beginning:
Our mission is to fight (food) waste by offering affordable and scalable packaging solutions that preserve products in the full supply chain.
Our products should give producers, processors and traders alike the assurance that their product is protected in the best manner possible. No more headaches about reducing quality, mould, insects and rejections and claims as a result.
At the same time, our solutions should be easy to integrate into the customer’s operation and form no restriction whatsoever.
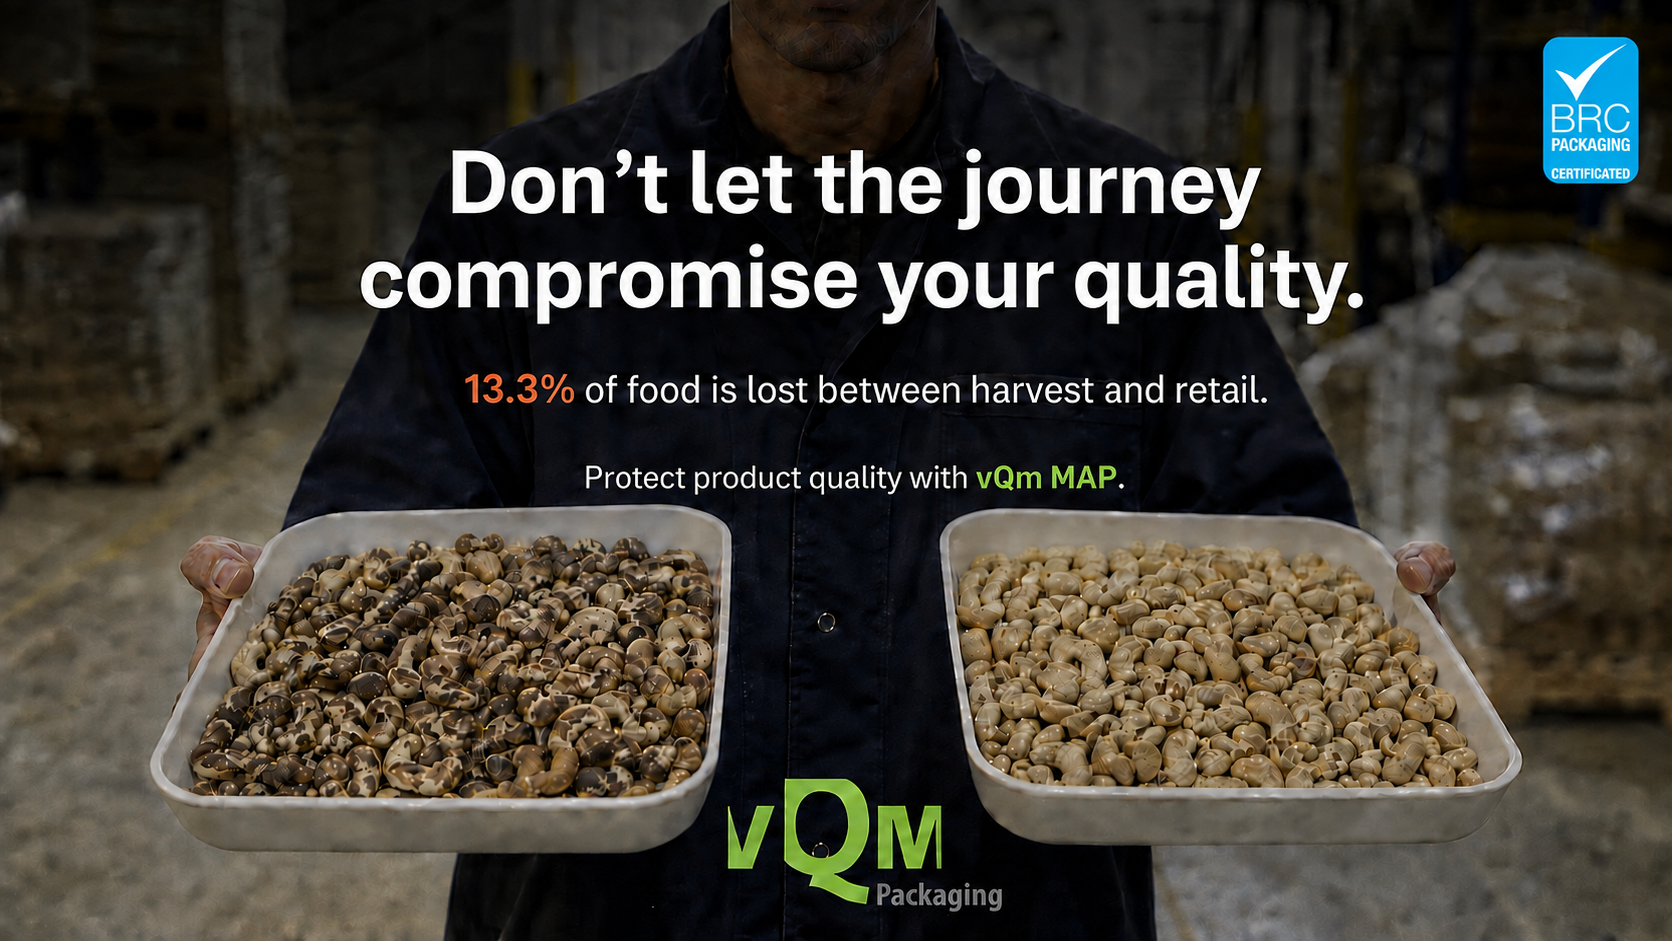
Around 13.3% of food is lost before it even reaches retail (FAO,2026). Part of that loss occurs during storage, transport and processing, where products can be exposed to moisture, oxidation, mould and insect infestation.
Many conventional semi-bulk packaging formats are designed primarily for handling and transport rather than long-term quality preservation. For high-value dry commodities, that can mean avoidable quality deterioration long before the product reaches its final customer.
Across the entire food chain, food loss and waste represent an economic impact of roughly USD 1 trillion every year (UNEP,2026) .
vQm aims to address a small but important part of that challenge. By protecting commodities with Modified Atmosphere Packaging, we help reduce avoidable quality loss, extend commercial shelf life and preserve more of the value already created at origin.
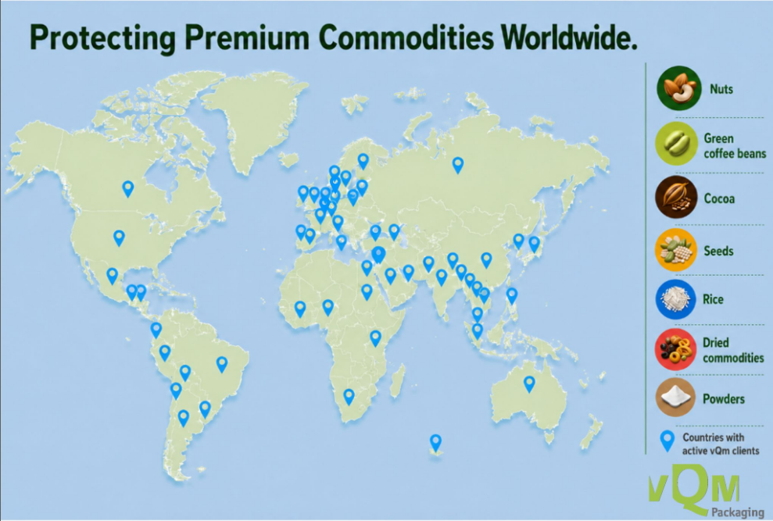
Today, vQm technology is used to support international supply chains in 48 countries worldwide, helping to protect valuable commodities during storage and transport.
From nuts, coffee and cocoa to grains, seeds, dried commodities, powders and industrial applications, vQm supports a wide range of products and supply chains around the world.
From local harvests to global markets, we help bridge the distance.
Founded in 2010, vQm Packaging builds on more than 50 years of expertise in controlling and modifying atmospheres within the CA Technology Group.
The group includes Van Amerongen CA Technology, together with specialist companies such as b-Cat High Altitude Training and Fontein, each applying controlled-environment technology within their own markets and applications.
Across the group, decades of experience in oxygen control, gas management, airtightness, measurement and environmental control are continuously shared and developed further.
vQm applies this expertise specifically to semi-bulk packaging, bringing Modified Atmosphere Packaging to big bags, pallet-sized liners and other packaging formats used in global supply chains.