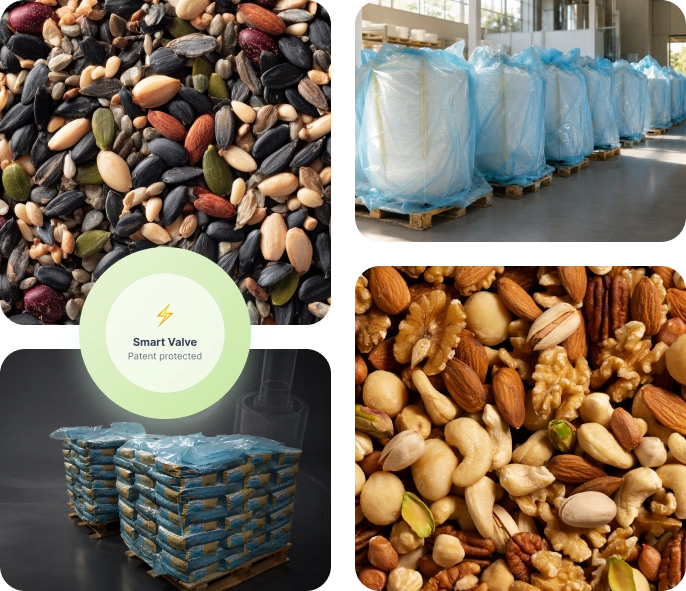
Engineered with extreme barrier technology, vQm completely protects your product against moisture, mould, oxidation, and pests. Fast, scalable, and engineered for pallet-sized shipments.
Modified Atmosphere Packaging helps preserve quality and extend shelf life of dry food commodities including nuts, grains, coffee, cacoa, tea, herbs, spices and powders.
Modified Atmosphere Packaging helps preserve seed quality, germination capacity and vigour during storage and transport.
Modified Atmosphere Packaging helps to eliminate insects across all life stages, without toxic fumigants.
Modified Atmosphere Packaging helps preserve quality and extend shelf life of chemicals, including hygroscopic powders, granulates and reactive compounds.
Vacuum volume reduction helps reduce the space required for storage and transport, while high-barrier packaging helps protect the product against oxidation and moisture.
Modified Atmosphere Packaging can also be applied to preserve other sensitive products that require protection against oxygen and moisture.
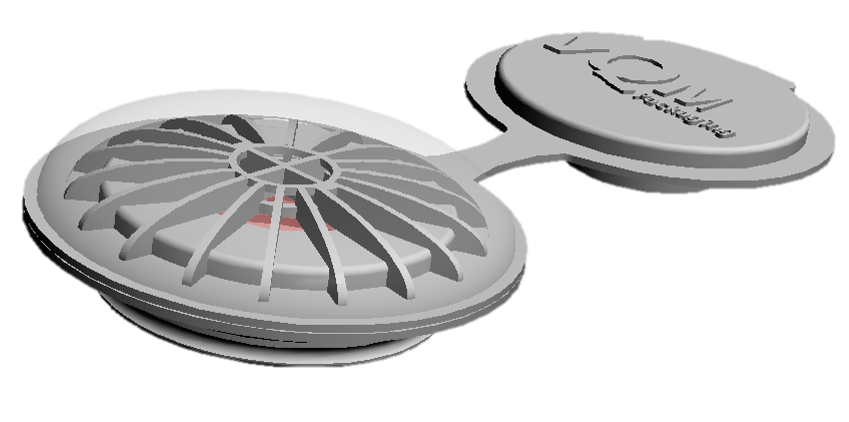
Our patented, smart valves allow for the most-efficient & lightning-fast gas flushing, incombination with vacuum cycles without compromising the bag’s integrity. The valves arecompatible with our stainless steel or aluminum head that can be securely connected to thevalve with a simple bayonet twist.Despite the flat and compact design, this small, user-friendly invention allows you to createoptimum & reliable protection for your product, at an unprecedented speed.Stay tuned for a new generation of valves that are on their way, with even more smart features!
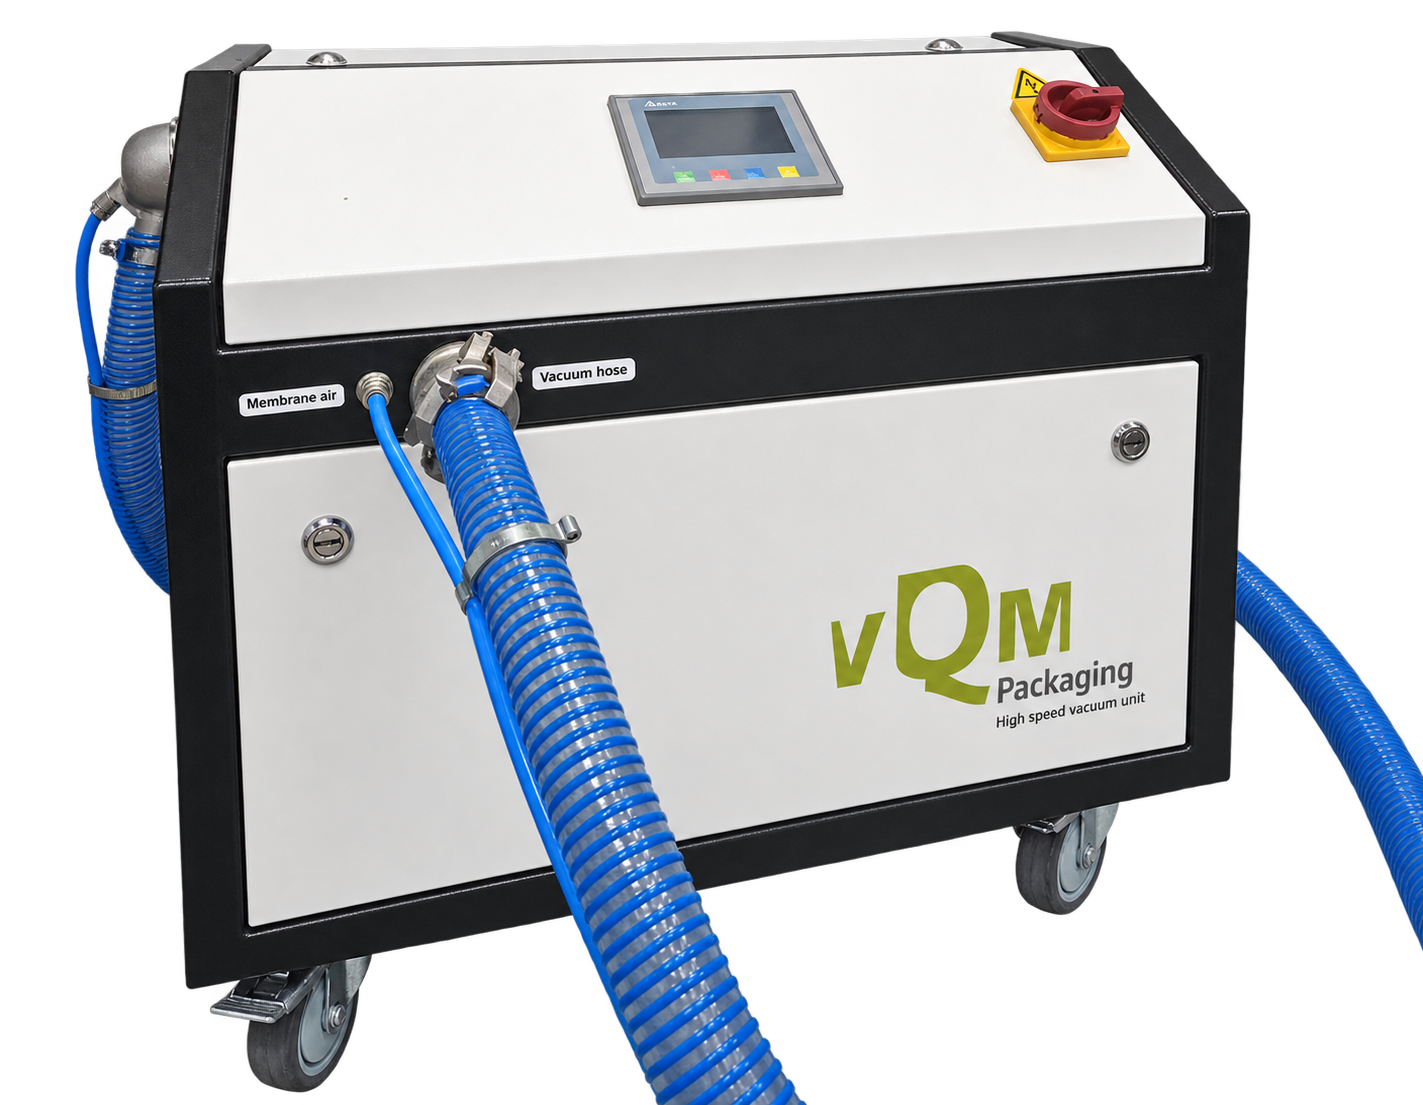
Our most commonly used High-Speed Unit operates on a 208–230 V, 50/60 Hz power supply. Itcan be programmed for modified atmosphere protocols using vacuum levels of up to 100 hPaabsolute.Most required MAP conditions can be achieved within one or two vacuum and gas-injectioncycles. Depending on the product, packaging, and selected protocol, the complete conditioningprocess normally takes approximately two to five minutes per pallet or big bag.Most users apply a protocol consisting of one combined vacuum and gas-injection cycle. Thisallows the injected gas to remain inside the packaging, minimizing unnecessary gasconsumption and waste.
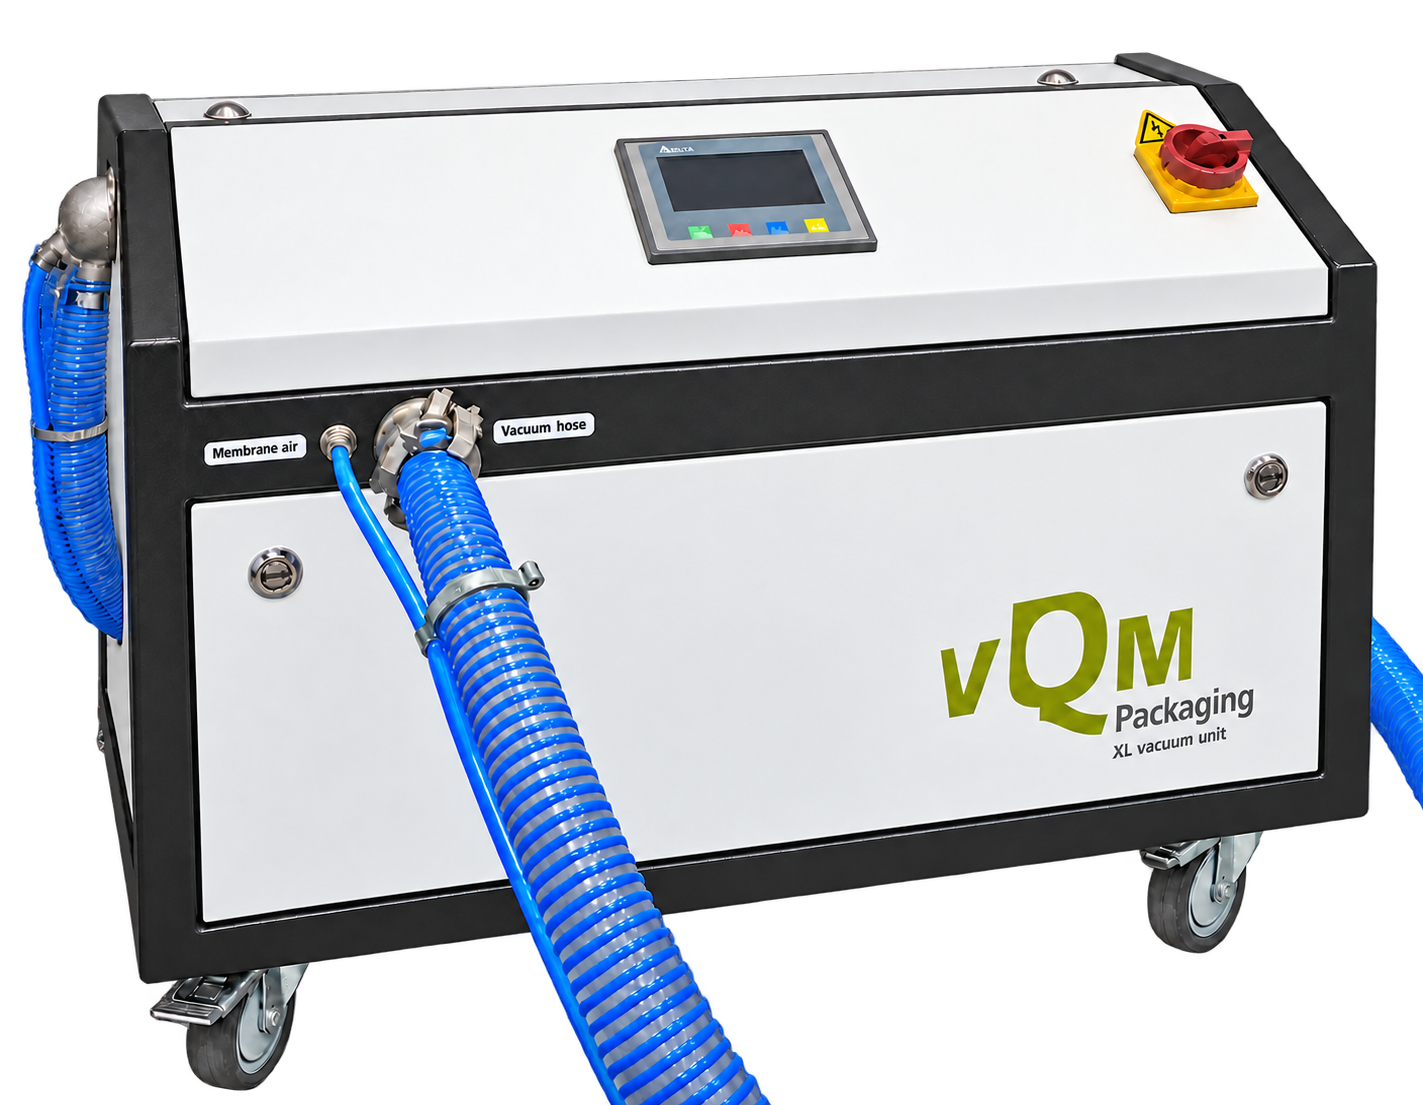
For more demanding conditioning protocols, the powerful vQm XL Unit provides the additional vacuum capacity required to achieve the desired conditions inside the packaging. This is particularly important for fine powders, which can restrict airflow through the product. Even in tall big bags filled with fine powders, the XL Unit can extract air from between the individual powder particles and achieve vacuum levels of up to 20 hPa absolute. As a result, a tall big bag filled with products such as milk powder can be conditioned to less than 2% residual oxygen in a single vacuum and nitrogen-injection cycle. With this compact system, operators can condition, seal, and secure a bulk big bag within minutes.
vQm Packaging is delighted to announce our presence at the…
We work closely with our customers before, during and after implementation to help ensure the vQm solution fits their product, process and operational requirements.
Our support continues beyond delivery, with practical assistance available whenever needed.
We aim to respond to technical questions, requests and enquiries within 24 hours on business days, helping you keep projects and decisions moving.
We only use premium brands (most from Germany) that are engineered to last and with a world wider network of service points (e.g. Becker Pumps, Bückert valves, Siemens control/touchscreen, Witt Gas sensors)
See the vQm system in action at our facility or join a live online demonstration. Test full semi-bulk packaging, ask technical questions and see vacuum, gas flushing and monitoring in real time.
Pilot trials can be performed to evaluate packaging, gas conditions and process settings for your specific product and application before full-scale implementation.
We provide practical training for operators, technical teams and quality assurance to ensure the vQm system is used correctly, safely, efficiently and delivers the required results. Training can cover equipment operation, packaging, sealing, MAP procedures and quality control.
Our team supports customers with product-specific questions, packaging selection, gas strategies, pilot trials and process optimisation. Whether you are implementing MAP for the first time, improving an existing process or dealing with a challenging commodity, we help determine the most suitable approach.
Our equipment is manufactured in-house at the vQm facility, allowing us to keep key systems and components in stock. Standard equipment orders can typically be prepared for shipment within two weeks.
vQm operates worldwide, supporting customers with implementation, training and technical guidance across international markets. In many regions, local partners are also available to provide additional support and selected services close to your operation, including insect treatment where applicable.