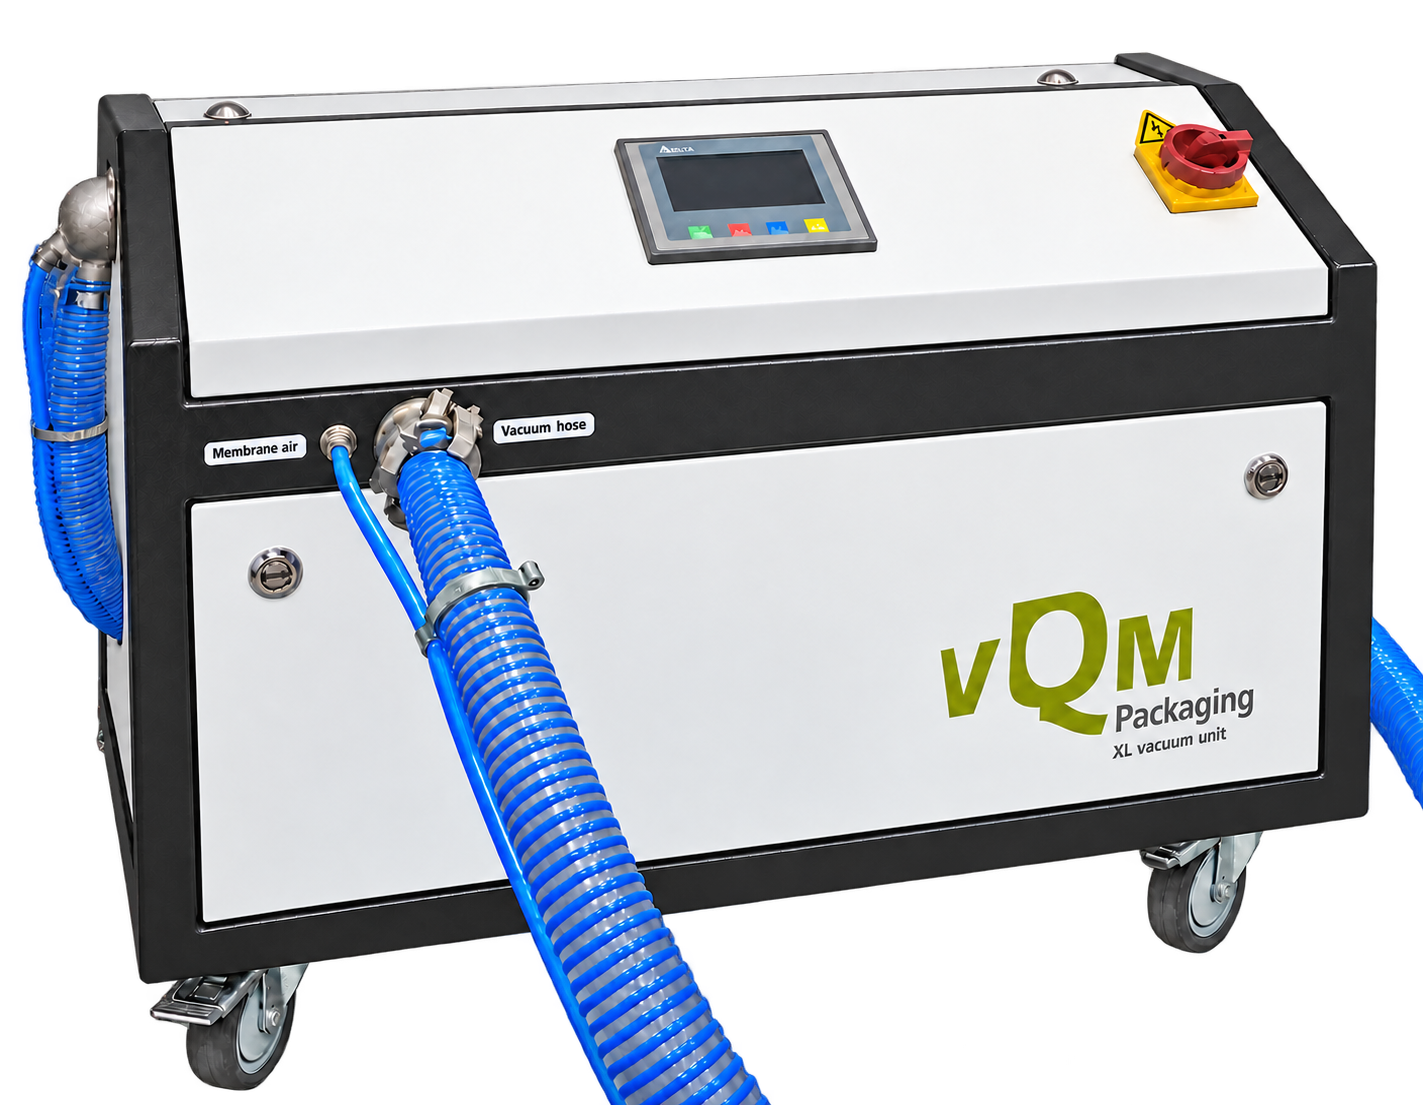
The vQm XL MAP Conditioning Unit is the high-power version of the High-Speed MAP Conditioning Unit, offering the same vacuum and gas-flushing functionalities with significantly increased vacuum capacity for demanding semi-bulk applications.
Equipped with a powerful 400V – 50/60Hz vacuum pump, the XL Unit is designed for products where air extraction becomes more difficult during vacuuming. This is particularly relevant for fine powders, dense products and other materials that compact under vacuum and restrict the free flow of air through the packaging. The XL version can reduce the oxygen concentration of typical (milk) powders inside MAP big bags, to less than 2% in just one combined vacuum and nitrogen injection cycle. By doing so, no nitrogen is wasted and fully used to protect your commodity. This makes the XL unit the most efficient ánd quickest post-gassing systems available on the market.
Combined with the patented vQm High-Speed Two-Way Valve, the XL Unit enables fast vacuum extraction and injection of nitrogen (N₂) or carbon dioxide (CO₂) through one secure connection point. Subsequent vacuum and gas-injection cycles can be used to efficiently create the required Modified Atmosphere Packaging conditions inside full big bags or pallet-sized high-barrier packaging, protecting products against external moisture, mold, oxidation and insects during storage and transport.
If the packaging is not equipped with the vQm High-Speed valve, the XL unit can be adapted for use with other types of access points as well, such as screw caps or similar connections. This makes the system highly flexible and allows it to be integrated with a wide range of existing packaging formats without requiring a standard vQm valve.
The vQm XL MAP Conditioning Unit is CE certified and designed for professional industrial use.
The powerful 400V vacuum system is specifically designed for dense products and fine powders where compacting material can restrict air flow during vacuum extraction.
Combined with the vQm High-Speed Two-Way Valve, the XL Unit enables rapid vacuuming and gas flushing of full semi-bulk packaging.
Creating and maintaining the required atmosphere inside high-barrier packaging helps reduce oxidation, external moisture ingress, mould-related risks and stored-product insect damage.
Low-oxygen or CO₂-enriched atmospheres can be used for stored-product insect control without applying conventional pesticide fumigants inside the packaging.
Despite its increased capacity, the XL Unit is designed for use at different packing locations and can be integrated into existing semi-bulk packaging operations.
Better storage protection can help preserve product quality for longer, providing more flexibility in deciding when products are stored, transported or sold.
The XL MAP Conditioning Unit works as part of a complete vQm packaging system.
All packaging is designed with the vQm valve sealed inside (that enables efficient gas flushing through one secure connection point at amazing speed), the packaging maintains the controlled atmosphere around the product after treatment.
The patented Two-Way Valve provides one secure connection point for both vacuum extraction and gas injection and allows the XL Unit to be connected quickly using a bayonet-style connection.
A reliable seal is essential for maintaining the required atmosphere after conditioning. The recommended sealing method depends on the selected packaging material and configuration.
The gas sensor can be used to measure the internal atmosphere and verify that the required O₂ and CO₂ concentrations have been achieved.
Suitable gas regulation equipment provides a controlled gas supply and helps prevent operational issues such as regulator freezing during high CO₂ flow rates.
The XL Unit offers the same basic vacuum and gas-flushing functionality as the High-Speed Unit but uses a more powerful 400V vacuum system. It is designed for demanding applications where product density or compaction restricts air flow during vacuuming.
Fine powders can compact around the packaging and valve during vacuum extraction, reducing the flow of free air. The higher vacuum capacity of the XL Unit helps maintain effective air extraction under these more demanding conditions.
Yes, the XL Unit can be used for a wide range of semi-bulk products where increased vacuum capacity, faster extraction or demanding packaging conditions require more power.
Yes, the unit can extract air and inject nitrogen (N₂) or carbon dioxide (CO₂) through the same vQm Two-Way Valve. Multiple vacuum and gas-injection cycles can also be programmed where required.
The system is designed for use with nitrogen (N₂), carbon dioxide (CO₂) or suitable gas mixtures, depending on the product and application objective.
Yes, the XL version uses a powerful 400V – 50/60Hz vacuum system and therefore requires a suitable industrial electrical connection.
Yes, the unit is designed for flexible industrial use and can be positioned at different packaging or production locations, subject to the required electrical and gas connections.
Yes, the XL Unit can create low-oxygen or CO₂-rich atmospheres used for stored-product insect treatment. The required treatment protocol depends on insect species, life stage, gas concentration, product temperature and exposure time.
The XL Unit is recommended when the product is particularly dense, fine or difficult to evacuate, when the material compacts strongly under vacuum, or when additional vacuum capacity is required to achieve the desired processing speed.
Create Modified Atmosphere Packaging and or vacuum conditions efficiently, even in dense powders and other challenging semi-bulk products.